Injection Molding
ORRO Manufacturing Co., Ltd. supplies custom injection molding for plastic and rubber parts when volume makes machining uneconomical. We tool and mold parts in POM, Nylon, PEEK, PP, PE and elastomers, matching gate and cooling design to the material so parts come out dimensionally stable and ready to assemble.
Materials We Mold
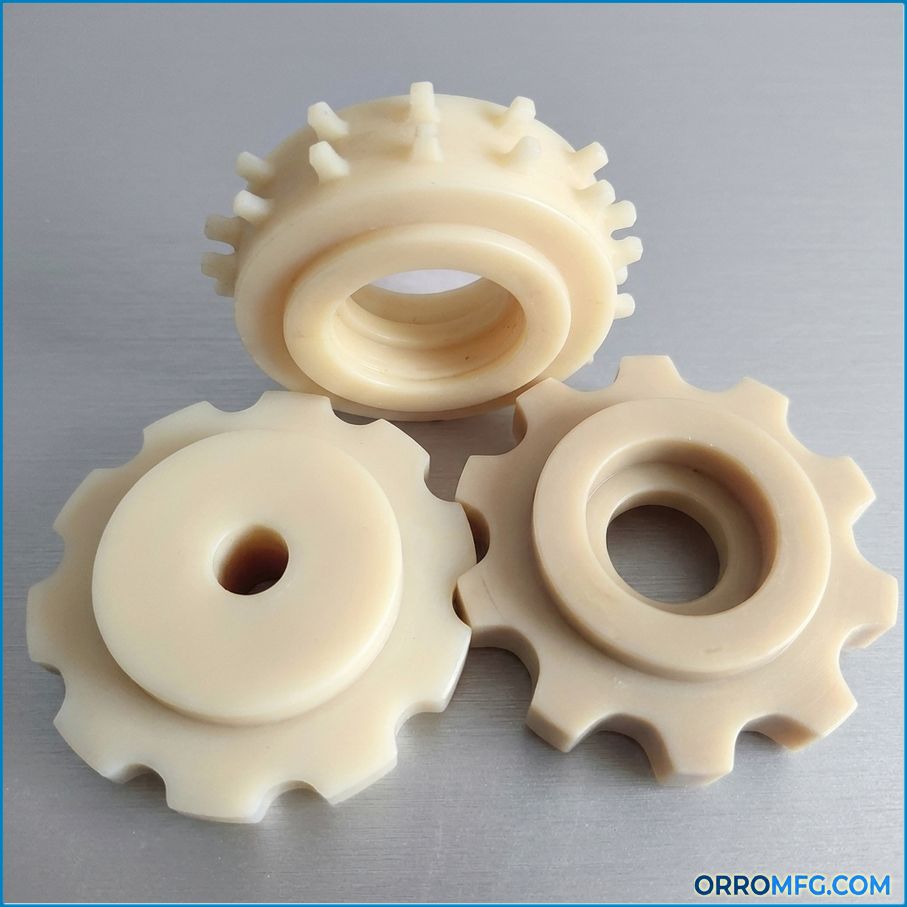
- POM (Delrin) — gears, cams, housings and precision parts
- Nylon (PA6/PA66) — tough structural parts and wear components
- PEEK — high-temperature and medical-grade parts
- PP, PE, ABS, PC — general and technical plastic parts
- Rubber and silicone — seals, gaskets and over-molded components
Specifications
- Tolerance: ±0.05 mm typical; tighter on critical features after tool qualification
- Tooling: prototype and production molds
- Volume: economical from a few thousand pieces upward
- Surface finish: SPI grades as specified
- Lead time: tooling 3–5 weeks, then production runs
Process Parameters
| Parameter | Typical value |
|---|---|
| Melt temperature | 200 – 400 °C (material dependent) |
| Mold temperature | 60 – 180 °C |
| Injection pressure | 800 – 1,500 bar |
| Holding pressure | 50 – 70% of injection pressure |
| Cycle time | 15 – 60 s |
| Clamp force | 50 – 250 t |
| Achievable tolerance | ±0.05 mm; tighter after tool qualification |
| Tooling | P20 / hardened steel, 1 – 16 cavities |
| Draft angle | 1 – 2° typical |
Applications
- Gears and cams — high-volume drive components
- Housings and covers — enclosures and structural parts
- Seals and gaskets — molded elastomer sealing parts
- Over-molded parts — rubber bonded to plastic or metal inserts
Case Studies
POM gears, 24-tooth, 8-cavity tool — an automation customer needed 24-tooth POM gears at ±0.05 mm in volume. We built an 8-cavity mold running a 30 s cycle, qualified the tool in 4 weeks and produced 50,000 gears per month, with first-article and periodic dimensional reports.
PEEK sealing rings, 4-cavity hot-runner tool — a semiconductor customer needed high-purity PEEK sealing rings at ±0.03 mm. We ran a 4-cavity hot-runner mold on a 45 s cycle, qualified the tool in 5 weeks and supplied 20,000 rings with full material traceability.
Related
- CNC machining or injection moulding? — the break-even volume, worked through with tooling cost
- Designing plastic parts for CNC machining — the features that are cheap to machine and expensive to tool