
CNC Machining
ORRO Manufacturing Co., Ltd. runs CNC machining as its core capability — 3-axis and 4-axis milling, CNC turning and 5-axis work for non-metallic parts that must hold tight tolerances without the corrosion and weight of metal. We machine engineering plastics, composites and graphite to your drawings, from one-off prototypes to production batches.
Materials We Machine
- PTFE — soft and chemically inert; needs sharp tooling and controlled feeds to avoid deformation
- PEEK — high strength and temperature resistance for medical, semiconductor and aerospace parts
- POM (Delrin) — dimensionally stable, ideal for gears, cams and precision slides
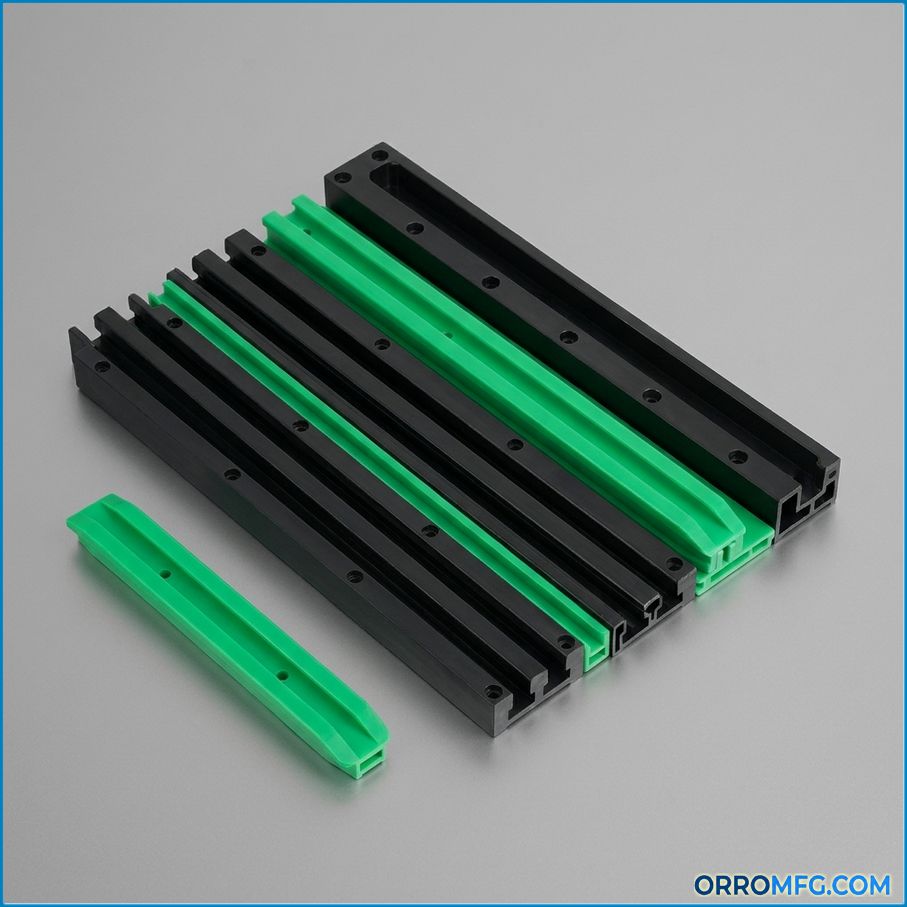
- Nylon (PA) — tough and wear resistant for bushings, rollers and guides
- PVC, PC, PP, UHMWPE — from rigid insulating parts to low-friction wear strips
- Graphite & FRP — machined with dust extraction and dedicated tooling
Specifications
- Tolerance: ±0.01 mm typical on critical features; ±0.05 mm general
- Surface finish: Ra 0.8 µm standard; Ra 0.4 µm on request
- Part size: up to 1200 mm envelope for milling; up to 300 mm diameter for turning
- Lead time: 2–3 weeks for prototypes and first articles
Machining Parameters
| Material | Cutting speed | Feed per tooth | Tooling | Notes |
|---|---|---|---|---|
| PTFE | 200 – 400 m/min | 0.05 – 0.15 mm | Sharp uncoated carbide, high rake | Air blast; avoid clamp marks |
| PEEK | 150 – 300 m/min | 0.05 – 0.12 mm | Micro-grain carbide, polished flutes | Stress-relieve before finish cut |
| POM | 300 – 600 m/min | 0.08 – 0.20 mm | Uncoated carbide | Clean chip formation, low burr |
| Nylon | 250 – 500 m/min | 0.08 – 0.18 mm | Sharp carbide, generous rake | Control moisture; air cool |
| UHMWPE | 400 – 800 m/min | 0.10 – 0.25 mm | Very sharp, polished | Light depths to avoid melting |
| Graphite | 150 – 300 m/min | 0.05 – 0.15 mm | Diamond-coated carbide | Dust extraction mandatory |
| PVC | 300 – 700 m/min | 0.10 – 0.20 mm | Polished carbide | Extract vapour; sharp edges |
| PC | 300 – 600 m/min | 0.08 – 0.18 mm | Sharp uncoated carbide | Anneal stock; air blast |
Applications
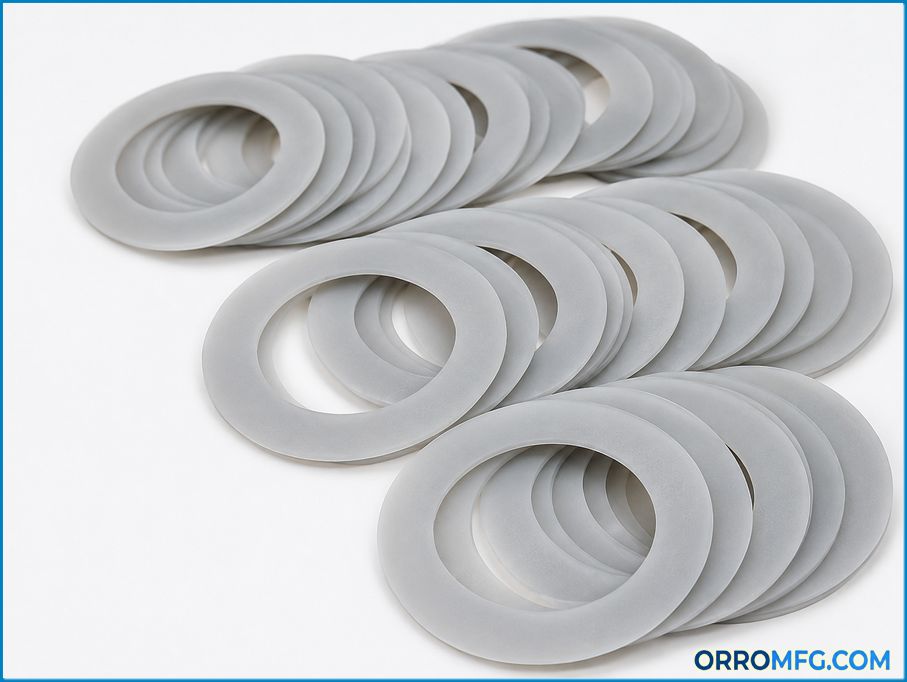
- Seals and gaskets — valve seats, diaphragms, piston rings and custom profiles
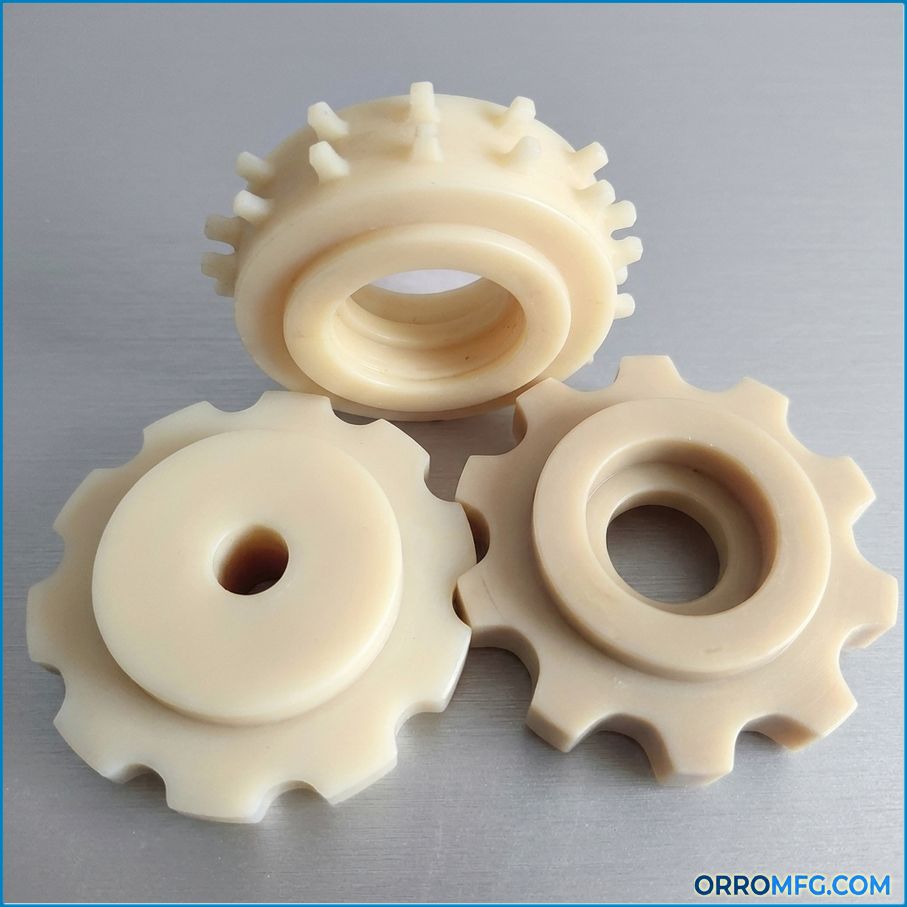
- Gears and sprockets — quiet, self-lubricating drives for automation and packaging
- Bushings and bearings — self-lubricating pivots and wear rings
- Insulating parts — dielectric spacers, standoffs and housings
Case Studies
PEEK wafer-handling end effectors — a semiconductor equipment builder needed end effectors with ±0.02 mm pocket depth and Ra 0.8 µm on sealing faces. We machined stress-relieved PEEK rod on a 4-axis mill, air-cooled with no liquid coolant, and verified every part on a CMM. 40 pieces shipped in 3 weeks with zero rework.
Graphite furnace fixtures — a heat-treatment customer needed 150 graphite load fixtures with ±0.05 mm slots and no coolant contamination. We machined them dry with dust extraction, deburred every edge and shipped in 2 weeks with a dimensional report per batch.
Related
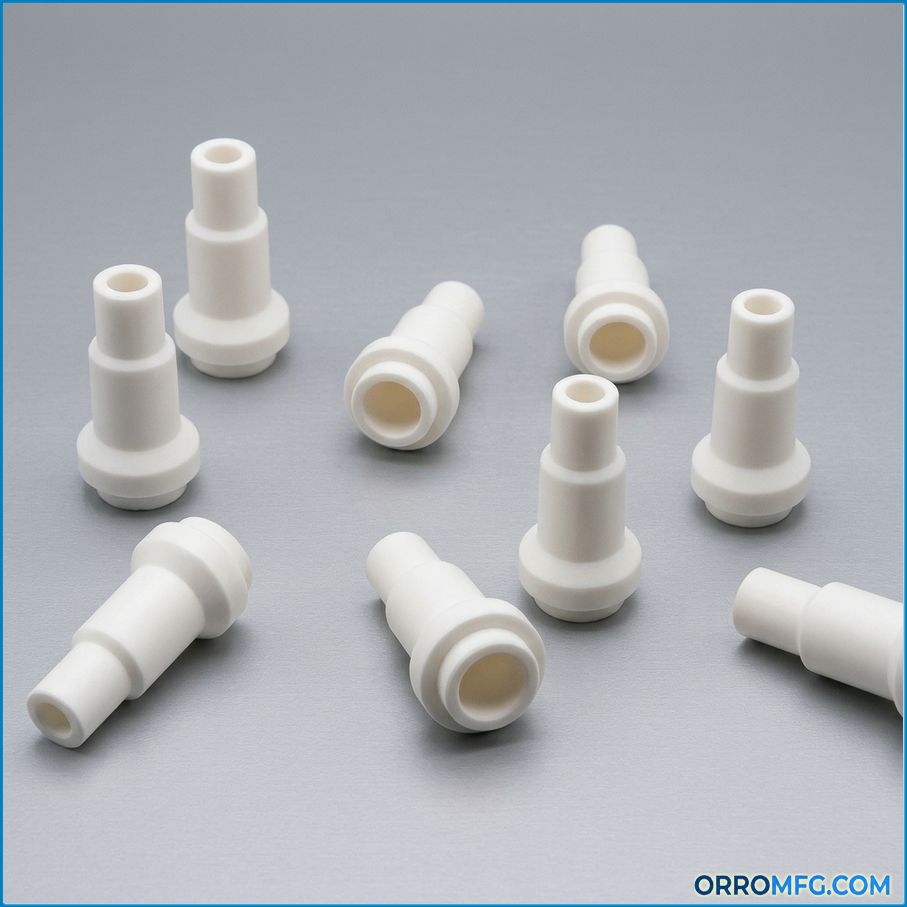
- Ceramic nozzles — alumina and zirconia parts ground and lapped after sintering
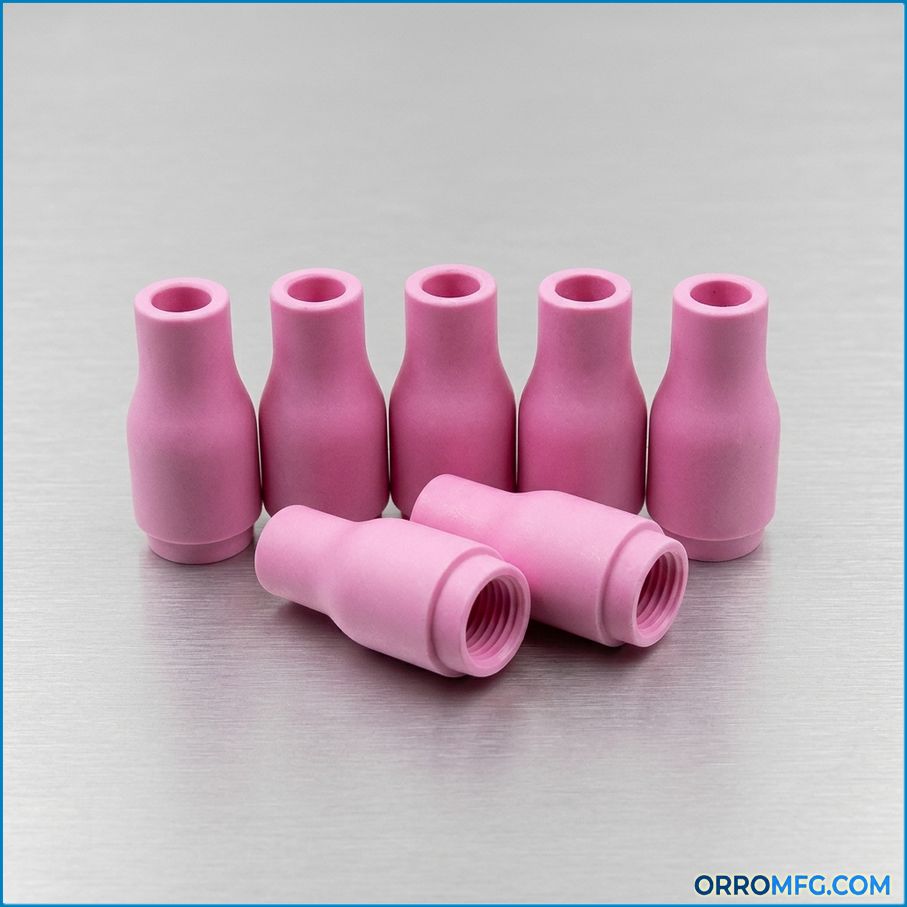
- TIG welding ceramic cups — the pressed-and-sintered form where the thread decides the fit
- POM machining — the plastic side of the same work, with the design rules that apply
Related Products
CNC Turning
Precision CNC turning services for cylindrical and rotational parts.
View →CNC Milling
CNC milling services for complex prismatic parts and prototypes.
View →5-Axis Machining
5-axis CNC machining for complex geometries and tight-tolerance parts.
View →Swiss Machining
Swiss-type CNC machining for small, high-precision turned parts.
View →