
Custom CNC Machined Plastic Parts
ORRO Manufacturing Co., Ltd. has been machining engineering plastics for more than 25 years, producing custom parts to drawing from one prototype to full production runs. CNC turning, 3/4/5-axis milling, laser cutting and wire EDM are all in-house, so a part that needs several operations stays under one quality system instead of being shipped between subcontractors.
The work is not difficult because of complex geometry — it is difficult because the material moves. Engineering plastics have high thermal expansion, low stiffness and a tendency to relax after cutting. Holding a bore at ±0.01 mm in POM, or a 0.5 mm wall in PEEK, depends on stress-relieved stock, correct feeds, sharp tooling and light finishing passes, not on the machine alone. That is the part of the job we specialise in.
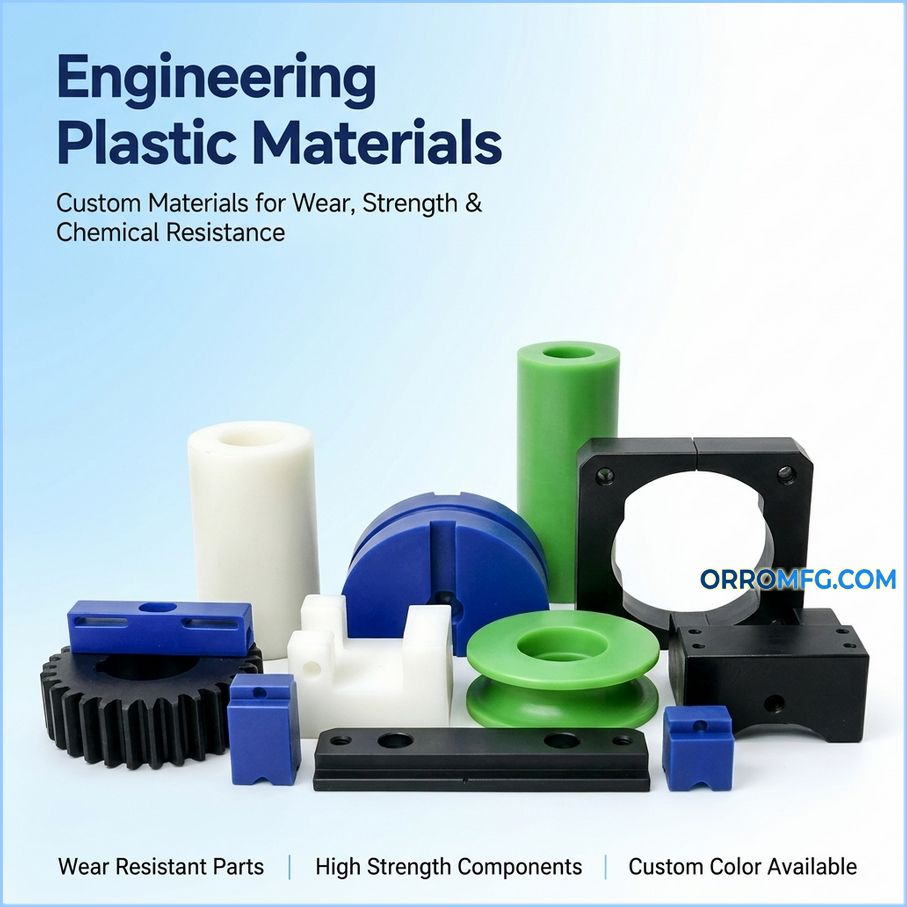
Materials We Machine
One material per application, chosen for what fails first: wear, chemical attack, temperature, weight or electrical insulation.
| Material | Typical machined parts | Chosen for |
|---|---|---|
| PTFE | Seals, gaskets, valve seats, diaphragms, piston rings | Near-universal chemical resistance, lowest friction, −200 to +260 °C |
| PEEK | Bushings, wear rings, insulators, bearing cages, gears | High strength at temperature, low outgassing, excellent wear |
| POM (Acetal) | Gears, cams, spacers, guide blocks, housings | Stiffness, dimensional stability, low friction against metal |
| Nylon (PA6 / PA66 / MC) | Bushings, rollers, sprockets, wear pads, thrust washers | Toughness, impact resistance, good bearing properties |
| UHMWPE / HDPE | Wear strips, chain guides, liners, star wheels | Abrasion resistance, low friction, no moisture absorption |
| PC | Guards, covers, insulators, light lenses | Impact strength and transparency |
| ABS | Housings, brackets, enclosures, prototypes | Easy machining, good surface, low cost |
| PVC | Insulating panels, duct parts, spacers | Rigid electrical insulation, flame-retardant grades |
| PP / PE | Tanks parts, chemical trays, covers | Chemical resistance at low cost |
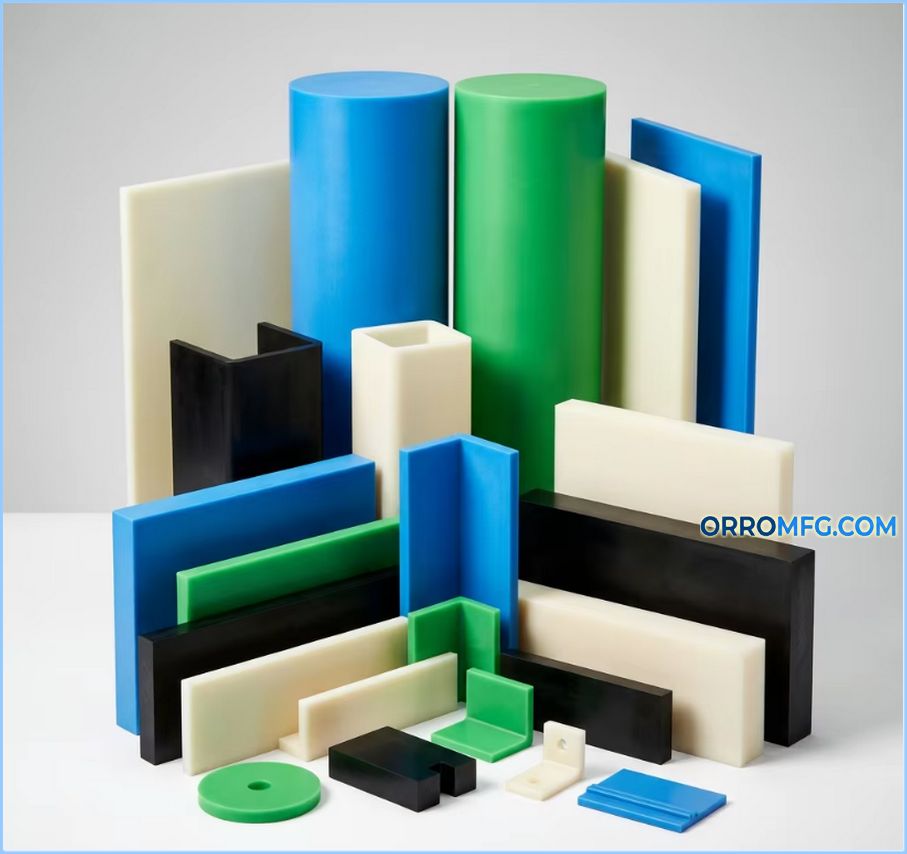
Capability Specifications
| Item | Scope |
|---|---|
| Turning | Ø 3–300 mm, up to 1,000 mm length; threads, grooves, tapers, bores |
| Milling | 3, 4 and 5-axis; pockets, slots, keyways, radii, drilled patterns, 3D surfaces |
| Maximum part size | Up to 1,200 mm in one piece (larger by assembly) |
| Tolerance | ±0.01 mm typical; tighter features reviewed case by case |
| Surface roughness | Ra 0.8 µm standard, Ra 0.4 µm on request |
| Minimum order | 100 pieces |
| Samples | 1–3 days |
| Production lead time | 7–14 days, depending on material and finishing |
| Drawing formats | STEP, IGES, STL, X_T, SolidWorks, UG, Creo, AutoCAD DWG/DXF, PDF |
| Documentation | Dimensional report, material certificate, first article inspection (FAI) |
| Confidentiality | NDA and exclusivity agreements signed on request |
On tolerance: ±0.01 mm is realistic on a machined plastic feature when the geometry allows it — a short bore, a small diameter, a flat face. Very thin walls, long unsupported bores and parts with large temperature swings need a tolerance review before quoting. We would rather say so at quotation than argue about it at inspection.
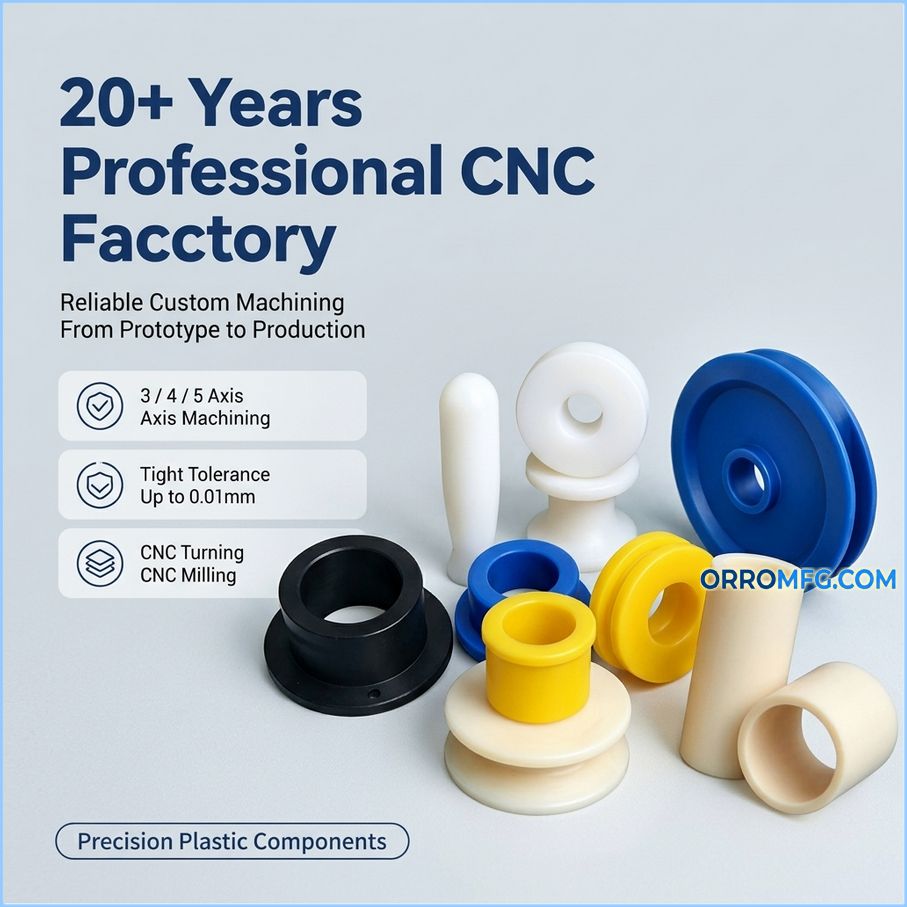
CNC Turning
Turning covers the round family: bushings, sleeves, spacers, collars, flanges, washers, rollers, threaded parts and small precision pins. Plastic turns differently from metal — it cuts as a continuous chip at high rake angles, and it will push away from the tool if the support is poor, so thin-wall parts are turned with soft jaws, light radial depth and a finishing pass that removes almost nothing.
Typical work: PTFE seal rings, POM bearing sleeves, nylon bushings, PEEK insulator bodies, UHMWPE rollers. Bores, groove widths and shoulder faces are inspected with pin gauges, bore gauges and micrometers, with CMM verification where the drawing calls for position or concentricity.
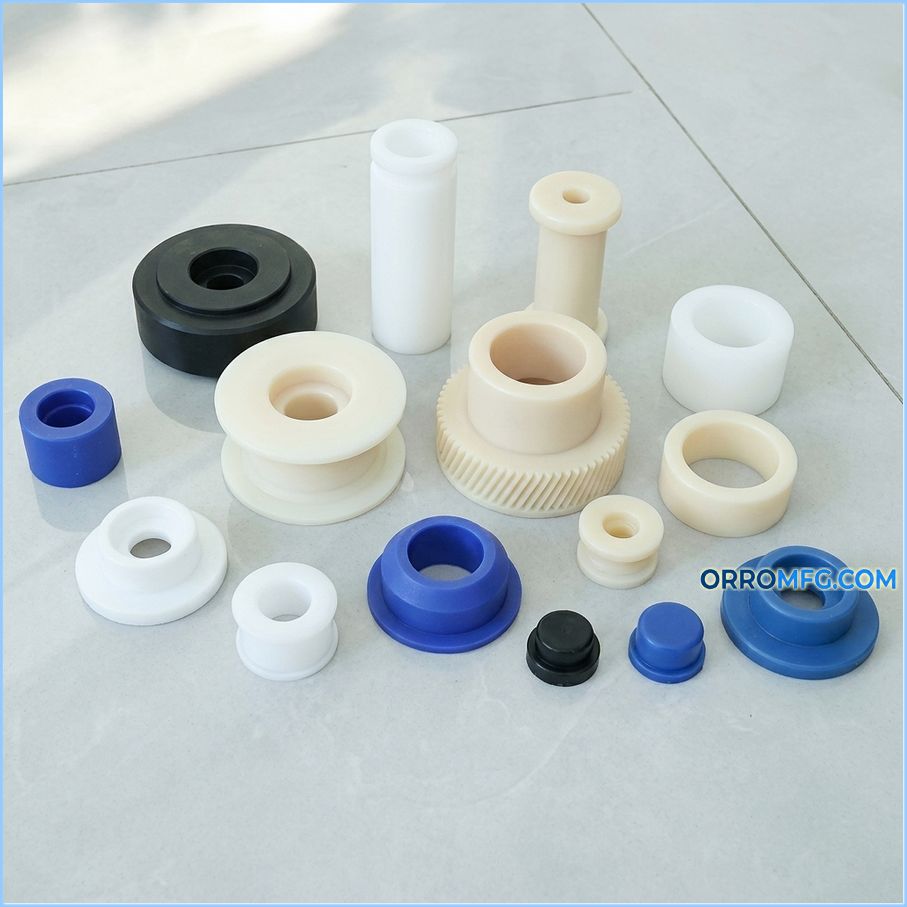
CNC Milling
Milling covers everything that is not round: brackets, mounting plates, housings, gear blanks, cam plates, keyways, pockets and drilled patterns. Multi-sided parts are set up on 4-axis fixtures where possible, which removes a second operation and keeps position tolerance between features instead of accumulating it.
Typical work: UHMWPE wear plates with counterbored holes, PVC insulating panels with milled slots, ABS instrument housings, POM cam plates, PEEK semiconductor fixture blocks.
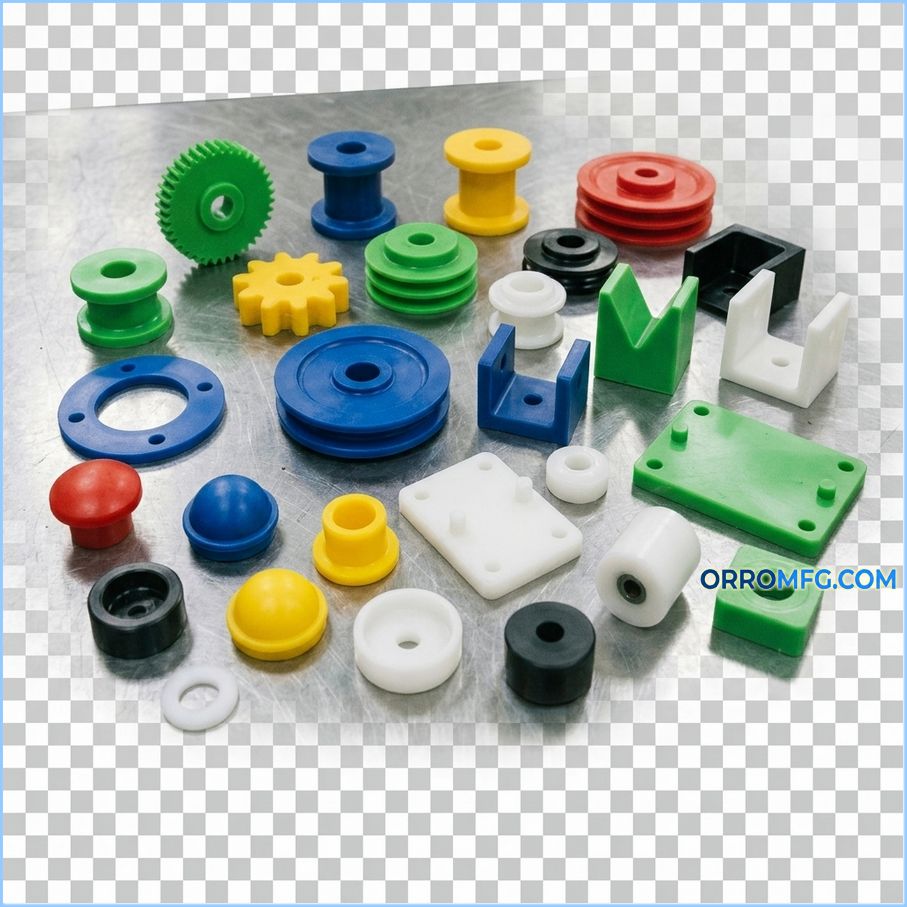
From Drawing to Finished Part
- Send the file — STEP, IGES, STL, DWG/DXF or a dimensioned PDF, or a physical sample. Multi-angle photos with key dimensions are accepted for simple parts.
- Engineering review — we check wall thickness, tolerances and features that are expensive to machine, and propose changes that save cost without losing function. No charge for this review.
- Quote — material grade, tolerance feasibility, finishing, tooling if needed, sample and production lead times.
- Sample — 1–3 days for most materials. You approve the sample before production.
- Production and inspection — parts run against the approved drawing, inspected, and shipped with a dimensional report and material certificate.
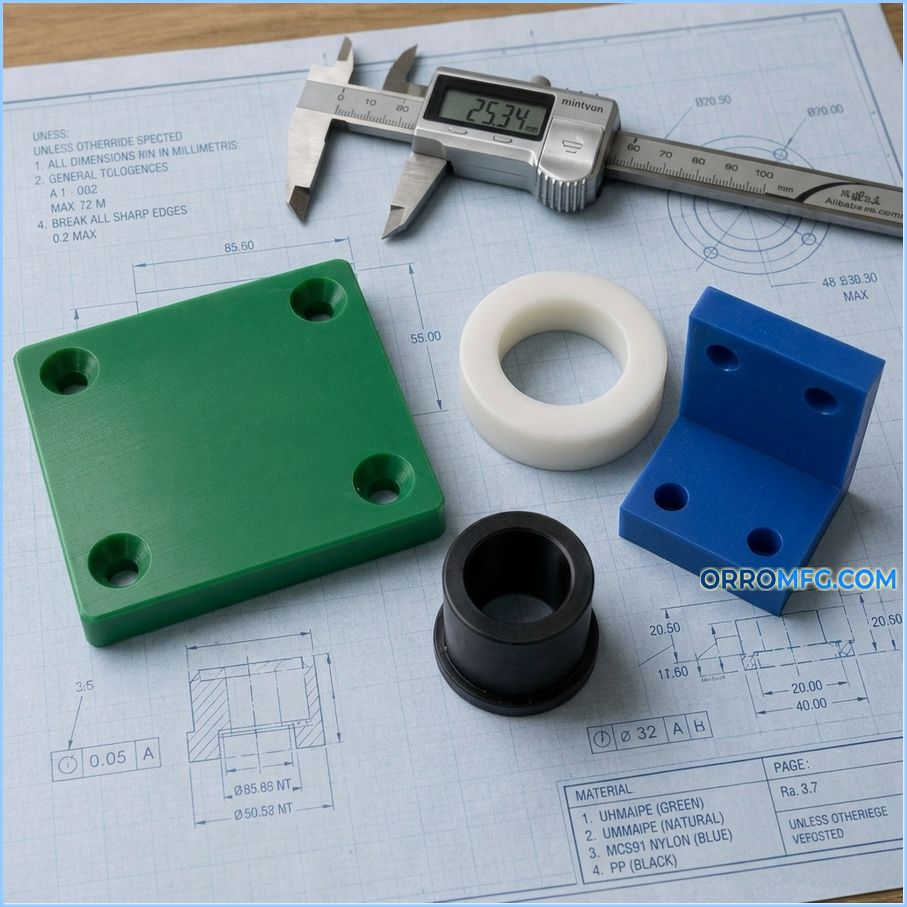
Quality Control
- Incoming material checked against mill certificates for grade, density and colour.
- First article inspection (FAI) on every new part before production release.
- In-process inspection against a control plan that names the gauge and sampling frequency for each critical feature.
- Final inspection with calibrated micrometers, bore and pin gauges, height gauges, radius gauges, roughness tester and CMM.
- Shipment documentation: dimensional report, material certificate, batch traceability, and PPAP-style documentation where the supply chain requires it.
- Manufacturing under an ISO 9001 quality management system, with RoHS-compliant materials.
Applications
- Industrial machinery — wear pads, guide blocks, cam plates, bushings, rollers, star wheels, chain guides.
- Electrical and electronic equipment — insulating panels, terminal spacers, fixture blocks, high-purity insulators.
- Automotive and transport — bushes, spacers, brackets, prototype housings, jigs and fixtures for assembly lines.
- Food and packaging lines — food-grade UHMWPE and POM parts, guide rails, change parts.
- Pumps, valves and fluid handling — PTFE seats, seals and diaphragms, PEEK wear rings, PVC pipe components.
- Prototyping and R&D — one-off functional prototypes in the final production material, not a substitute.
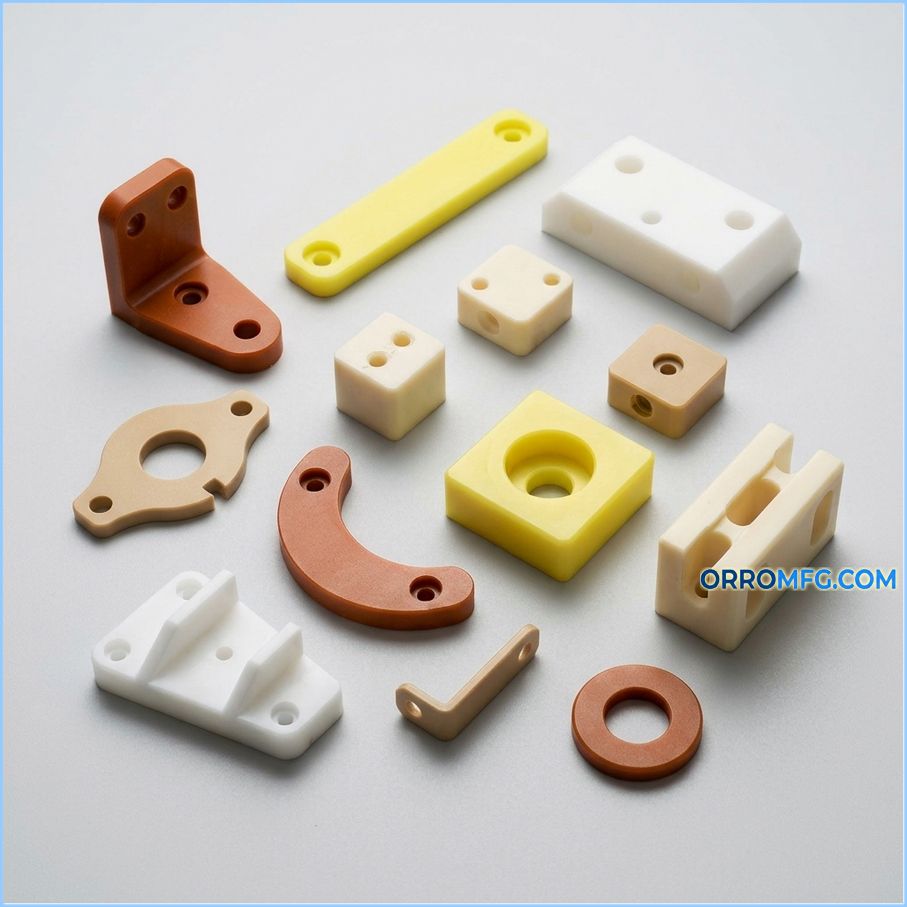
Case Studies
PEEK insulating bushings, 0.5 mm wall — a switchgear maker needed PEEK bushings with a 0.01 mm bore and a 0.5 mm wall, which tends to collapse if machined hot or gripped hard. We annealed the stock, used soft jaws and light finishing passes, and shipped 2,000 pieces with a dimensional report per batch.
PVC insulating panels, 1,000 mm — an electrical panel builder needed PVC insulating panels up to 1,000 mm with milled slots and clean edges. We machined them with dust and vapour extraction, deburred the edges and shipped 300 panels in 3 weeks.
Frequently Asked Questions
What is the minimum order quantity?
100 pieces per part number. Smaller quantities — a prototype, a replacement part or a single fixture — are quoted as sample orders, because the part is cut from stock and there is no tooling to amortise.
How fast can I get a sample?
1–3 days for most materials and simple geometry, and 7–14 days for production quantities. If the part needs a secondary operation or a special grade we do not stock, we tell you the real date at quotation instead of after the order.
Can you machine metal as well?
Our focus is engineering plastics and elastomers, and that is where our process knowledge and tooling are set up. Metal parts are better placed with a metal shop. We do supply plastic-to-metal assemblies where the metal component is bought in and the plastic part is machined here.
How do you hold ±0.01 mm in a material that expands?
Three things: stress-relieved stock so the part does not move after machining, temperature-stable inspection (parts measured at 20 °C, not straight off the machine), and light finishing cuts with sharp tooling. Where the geometry cannot support that tolerance — very thin walls, long unsupported bores — we say so before quoting rather than after.
Will you sign an NDA?
Yes. Non-disclosure and exclusivity agreements are signed on request, before drawings are shared. Your drawings are not reused for other customers and are not published.
What documentation comes with the parts?
A dimensional inspection report and a material certificate as standard. First article inspection reports, PPAP-style documentation and batch traceability are available where your supply chain requires them.
Can you match a colour?
Yes for most plastics — natural, black, white and standard colours are stocked, and custom colour matching is available on PVC, ABS, PP and POM where the mill offers it. Colour is a material property, so it affects lead time rather than machining cost.
Related Products
- PTFE Custom Machined Part — chemical-resistant machined components
- POM CNC Machined Parts — acetal parts to drawing
- Nylon Bushing — wear-resistant nylon bearings
- PEEK Self-Lubricating Bushing — high-temperature bearing parts
- UHMWPE Wear Strip — low-friction abrasion-resistant strips
- Designing Plastic Parts for CNC Machining — design rules that cut cost
- CNC Machining Processes and Tolerances — what each process can hold
Send your drawing for a same-day quote. Attach the 2D or 3D file, tell us the quantity and the working conditions, and our engineering team will reply with material grade, tolerance review and lead time.